
Common Problems and Solutions of Bolt Fasteners during Installation
Bolt fasteners hold flanged joints, pressure vessels and structural steelwork together, and most field failures begin at installation rather than in service. The four recurring problems — loosening, thread damage, unsuitable material and a wrong tightening sequence — are preventable when the joint is designed, assembled and inspected as one system, including the flange gaskets and the bolting that complete the connection.
Why Bolts Loosen and How to Prevent It
Vibration, thermal cycling and creep in the contact zone all relax preload. When the clamping force falls below the level that keeps the seating surfaces pressed together, the joint starts to move and the bolt backs off.
- Locking nuts and prevailing-torque nuts add friction in the thread so it resists rotation under vibration.
- Locking washers with serrations or a spring profile increase friction and stop the nut turning.
- Thread-locking compounds cure in the thread gap and prevent self-loosening without changing the bolt grade.
- Periodic re-torque checks with a calibrated torque wrench confirm that preload is still present.
Cleanliness and lubrication matter too. Grit left in the joint acts like a spring and lets preload decay, while one consistent lubricant keeps friction repeatable from bolt to bolt.
Thread Damage: Causes and Detection
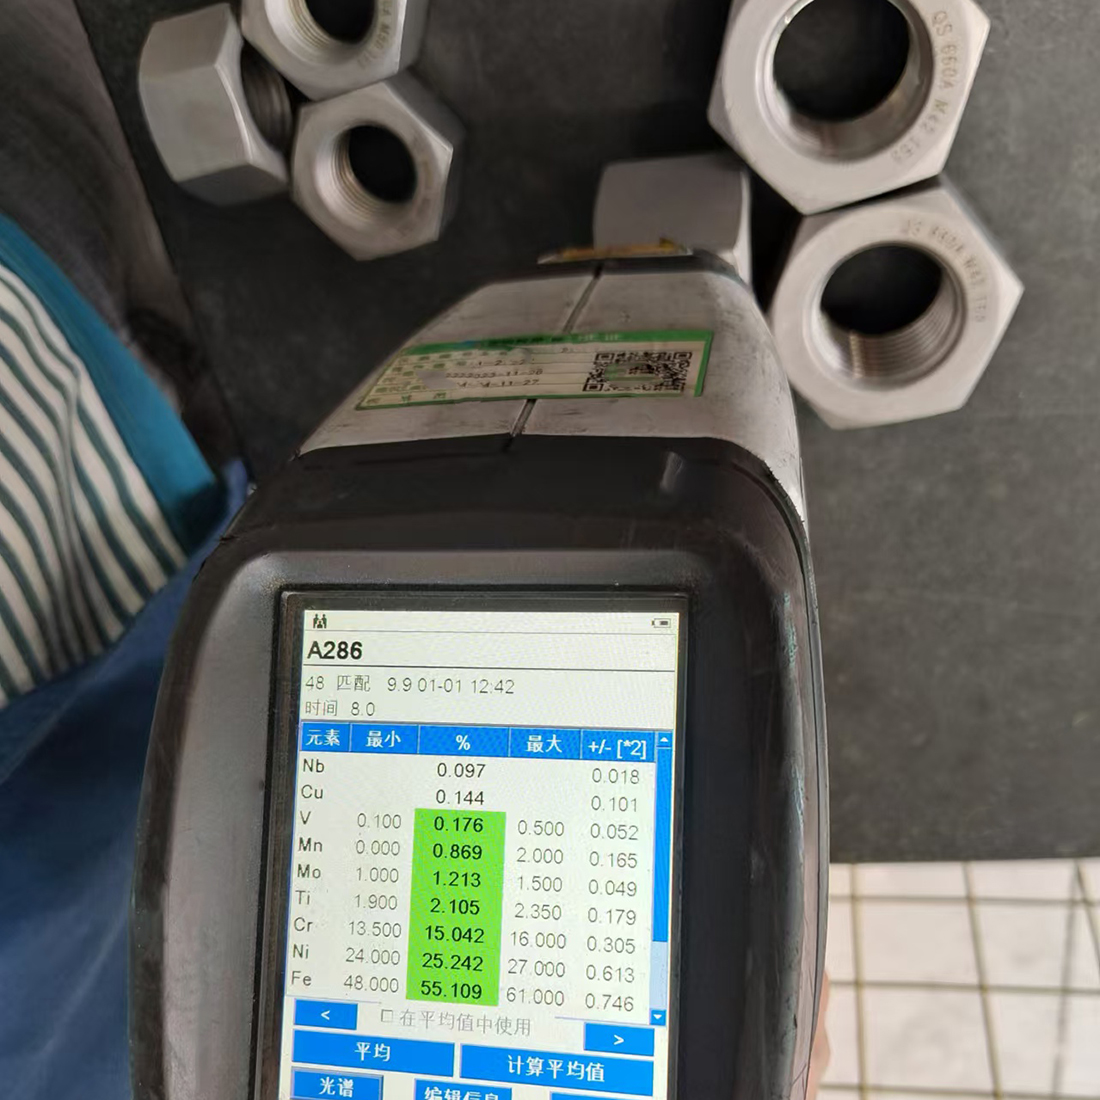
Stripped, galled or deformed threads come from wrong torque, mismatched thread pitch, worn tools or poor material quality. A damaged thread does not hold preload and can fail the whole joint, so inspect every stud and nut before assembly.
- Visual inspection — look for wear, nicks, rust and deformation, and check that the thread surface is clean and dry.
- Thread gauges — a go/no-go gauge checks pitch and diameter against the standard.
- Caliper and micrometer measurement — verify major diameter, pitch and thread depth against the drawing.
- Non-destructive testing — ultrasonic and magnetic particle methods reveal internal and surface cracks.
- Preload and torque tests — confirm the bolt still holds the specified torque without creeping.
Replace damaged stud bolts instead of re-threading them on site. A repaired thread rarely returns to its original fit, and the joint keeps the risk.
Selecting the Right Bolt Material
Material follows service conditions: temperature, corrosion exposure and load. Stainless steel, carbon steel and alloy steel cover most duties, but the grade must match the medium and the design temperature.
- Strength — tensile and yield strength must cover the design load with margin.
- Corrosion resistance — in wet, chemical or marine exposure use stainless or coated bolts, for example hot-dip galvanized steel.
- Temperature — high-temperature service needs thermal stability; low-temperature service needs toughness to avoid brittle fracture.
- Weight and cost — match material density and price to the project budget without cutting performance.
- Machining and heat treatment — free-machining grades lower production cost, while heat-treatable grades allow higher strength after treatment.
Common combinations such as ASTM A193 B7 studs with ASTM A194 2H nuts show how strength and hardness are matched inside one joint.
| Factor | What to check | Selection outcome |
|---|---|---|
| Strength | Tensile and yield strength against the design load | Bolt sized with margin against yielding |
| Corrosion | Medium, humidity, chloride exposure | Stainless or coated bolt selected |
| Temperature | Design minimum, maximum and cycling | Thermal stability or low-temperature toughness |
| Cost and machining | Volume, tolerances, heat treatment | Free-machining grade or treated grade |
Note: values are indicative; confirm the fastener grade and the standard called out on the drawing.
Correct Installation and Tightening Sequence
Installation errors — a wrong tightening sequence, uneven torque or a mismatched bolt length — create stress concentration and let the joint relax. Follow the manufacturer's tightening procedure and train the crew that performs the work.
- Cross pattern — bring bolts to seating torque in stages and in opposite pairs so the gasket and the pipe flanges compress evenly.
- Even torque application — a calibrated torque wrench with the specified lubrication spreads load across the joint.
- Correct hardware — match bolt length and diameter to the flange thickness, and use the nut grade specified for the bolt.
- Post-installation check — verify torque after the pressure test or the first thermal cycle and record it.
Recording bolt grade, torque value and inspection date turns a one-off repair into a traceable maintenance routine.
Frequently Asked Questions
Why do bolts loosen even when they were torqued correctly?
Vibration, temperature change and creep reduce preload over time. Locking hardware, thread-locking compounds and periodic re-torque checks keep the clamping force stable.
How do I check thread damage before installation?
Start with visual inspection, then use a go/no-go thread gauge and caliper measurements; for critical joints add ultrasonic or magnetic particle testing.
Which bolt material suits high-temperature service?
Choose an alloy steel grade with thermal stability and creep resistance, and confirm the temperature range given in the fastener standard.
Can I reuse bolts after a joint is opened?
Bolts showing necking, thread damage or corrosion should be replaced. If the fastener standard allows reuse, re-check dimensions and torque before assembly.
Development of high temperature alloy materials
660 stainless steel standard and application
Related Article


